Back to All Consumables & Supplies
EN 10204 3.1 Certified • Full Heat Traceability
Welding Filler Wires, Electrodes & Tungsten
Code-approved welding filler wires and electrodes backed by authentic EN 10204 Type 3.1 mill test certificates. Guaranteed chemistry, smooth arc stability, and radiographic soundness across GTAW, GMAW, and SMAW.
Annexure-1 Items: 8 Verified Products
Dispatch Hub: Sector-20, Ulwe, Navi Mumbai
QA Vetting: CSWIP 3.1 • EN 10204 3.1
Annexure-1 Dimensional & Size Schedule
8 items cataloged| Item # | Item Description | Size / Dimension | Grade / Brand Ref | MTR Status |
|---|---|---|---|---|
| #49 | Filler Wire SS 316L (Dia 1.6 mm) | Dia 1.6 mm x 1000 mm Length (TIG Rod) | Annexure-1 / Certified SS 316L | EN 10204 3.1 |
| #40 | Filler Wire SS 316L (Dia 2.0 mm) | Dia 2.0 mm x 1000 mm Length (TIG Rod) | Annexure-1 / Certified SS 316L | EN 10204 3.1 |
| #39 | Filler Wire SS 316L (Dia 2.5 mm) | Dia 2.5 mm x 1000 mm Length (TIG Rod) | Annexure-1 / Certified SS 316L | EN 10204 3.1 |
| #50 | ER 70S-6 Filler Wire (MIG Wire) | Dia 0.8 mm / 1.2 mm (15 kg Spool) | Annexure-1 / Industrial MIG Grade | EN 10204 3.1 |
| #52 | ER 70S-2 Filler Wire (TIG Rod / Electrode) | Dia 1.6 / 2.0 / 2.4 mm x 1000 mm Length | Annexure-1 / Certified TIG Grade | EN 10204 3.1 |
| #51 | E 7018 Heavy Duty Welding Electrode | Dia 2.5 mm / 3.15 mm / 4.0 mm x 350/450 mm | Annexure-1 / Low Hydrogen Grade | EN 10204 3.1 |
| #36 | Tungsten Rod (TIG Electrode) - 2.4 mm | Dia 2.4 mm x 175 mm Length | Annexure-1 / Precision Tungsten | EN 10204 3.1 |
| #37 | Tungsten Rod (TIG Electrode) - 3.0 mm | Dia 3.0 mm x 175 mm Length | Annexure-1 / Precision Tungsten | EN 10204 3.1 |
Individual Product Profiles & Specifications
8 verified industrial items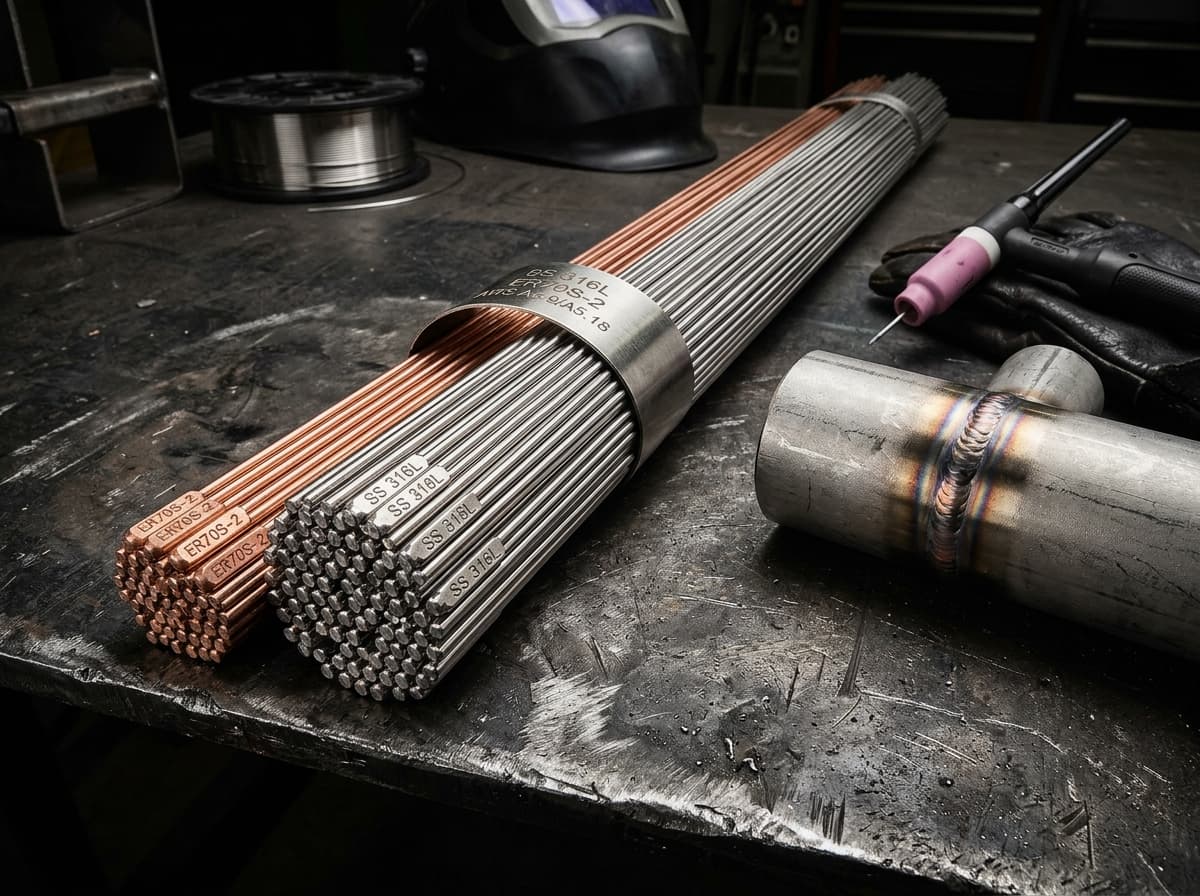
Fast Moving
Welding Filler Wires
Filler Wire SS 316L (Dia 1.6 mm)
AWS A5.9 ER316L stainless steel TIG filler rod (Dia 1.6mm) for precision root pass welding.
- Superior resistance to intergranular corrosion and pitting in chloride media
- Smooth arc transfer with high puddle fluidity under pure argon shielding
- Both ends stamped with grade 316L for permanent positive identification
Fast Moving
Welding Filler Wires
Filler Wire SS 316L (Dia 2.0 mm)
AWS A5.9 ER316L stainless steel TIG filler rod (Dia 2.0mm) for hot and fill pass welding.
- Clean drawn finish free of drawing grease, rust, and surface defects
- Radiographic quality weld deposits conforming to ASME Section IX
- Excellent mechanical toughness at ambient and cryogenic temperatures
Fast Moving
Welding Filler Wires
Filler Wire SS 316L (Dia 2.5 mm)
AWS A5.9 ER316L stainless steel TIG filler rod (Dia 2.5mm) for high deposition cap passes.
- High deposition rate reducing total arc-on time on thick welds
- Controlled delta ferrite number (4 to 10 FN) preventing hot cracking
- Low spatter and excellent bead wetting at bevel side walls
Fast Moving
Welding Filler Wires
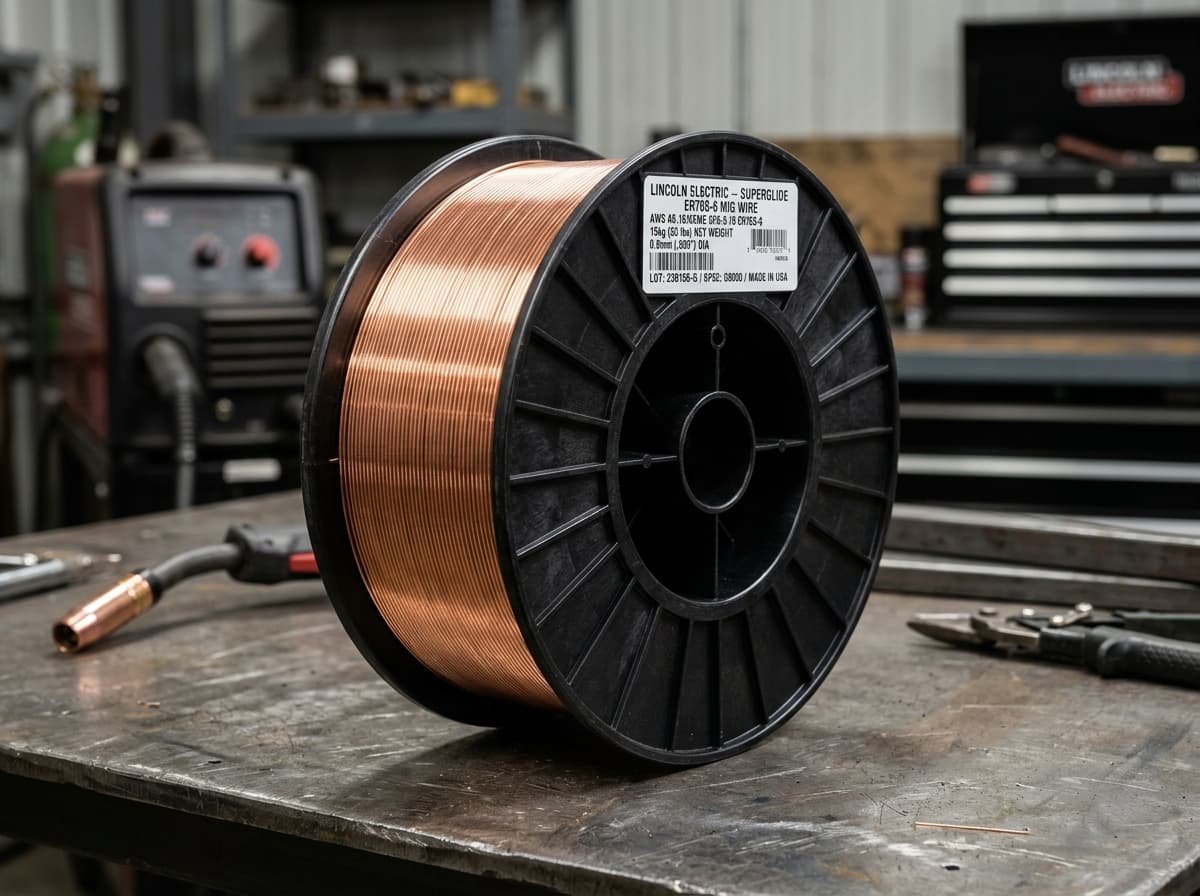
ER 70S-6 Filler Wire (MIG Wire)
AWS A5.18 ER70S-6 high-deoxidizer copper-coated solid MIG wire for carbon steel fabrication.
- Smooth wire feeding with zero copper flaking in liners
- High silicon content creates clean, flat weld beads with wash-in edges
- Approved for structural steel, heavy skids, and automotive chassis
Fast Moving
Welding Filler Wires
ER 70S-2 Filler Wire (TIG Rod / Electrode)
AWS A5.18 ER70S-2 triple-deoxidized TIG rod for high-pressure carbon steel pipe root passes.
- Eliminates porosity even on rusty or scaled pipe joints
- Produces clean, mirror-smooth root passes passing 100% radiography
- Meets ASME Section I & B31.3 high-pressure piping specifications
Fast Moving
Welding Filler Wires
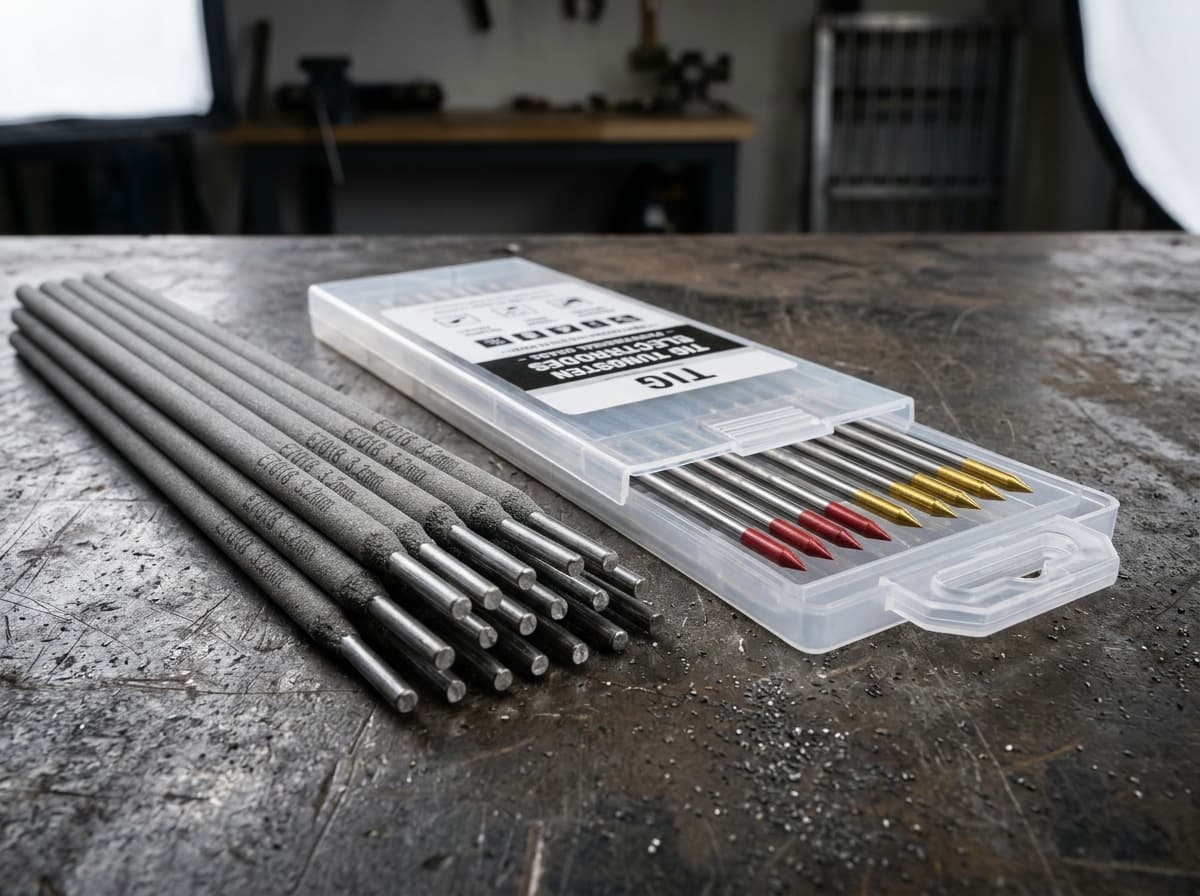
E 7018 Heavy Duty Welding Electrode
AWS A5.1 E7018 iron-powder low-hydrogen electrode (H4) for structural steel & heavy machinery.
- Extremely low moisture absorption coating resisting hydrogen cracking
- Stable arc with minimal spatter and easily detachable slag
- All-position capability: flat, vertical-up (3G), and overhead (4G)
Fast Moving
Welding Filler Wires
Tungsten Rod (TIG Electrode) - 2.4 mm
Ground-finish 2.4mm Tungsten electrode (EWTh-2 / WL15) for high-current TIG fusion welding.
- Superior arc ignition and restriking performance
- Low burn-off rate with resistance to thermal erosion
- Maintains pinpoint arc column for deep root penetration
Welding Filler Wires
Tungsten Rod (TIG Electrode) - 3.0 mm
Heavy 3.0mm Tungsten electrode for high-amperage TIG welding and heavy plate joints.
- Handles heavy thermal loads without balling on DCEN
- Low contamination risk into molten weld puddle
- Certified 100% eddy-current tested for zero internal fissures
Technical Documentation • Annexure-1 Engineering Standards
Engineering Notes for Welding Filler Wires, Electrodes & Tungsten
Quality Assurance, Heat Traceability & EN 10204 3.1 Certificates
In high-integrity engineering applications across Navi Mumbai, Taloja, Rabale, and Maharashtra fabrication corridors, consumable quality directly dictates weld longevity and safety. MechSure Engineering guarantees that all supplied welding wires, electrodes, abrasives, and chemical sealing products are authenticated against mill test certificates (MTR).
Every batch of SS 316L filler wire, ER 70S-6 MIG spools, and E 7018 basic low-hydrogen electrodes is traced by heat number, documenting exact chemical composition (C, Mn, Si, P, S, Cr, Ni, Mo, N) and mechanical properties (Tensile strength, Yield strength, Elongation %, and Charpy V-Notch impact values at -30°C or -46°C).
Applicable Codes:AWS A5.9, AWS A5.18, AWS A5.1, ASME Section II Part C, EN 10204 3.1/3.2, IS 814.
Handling, Storage & Shop-Floor Best Practices
Proper storage and application discipline ensure peak consumable performance. Low-hydrogen E 7018 electrodes must be maintained in holding ovens at 120°C to 150°C after re-baking to prevent hydrogen-induced cold cracking (HICC) in high-strength structural joints.
For stainless steel cutting and grinding, our cutting wheels (125 x 3.2, 180 x 2.8, 100 x 1.0) are strictly formulated free of iron, sulfur, and chlorine (< 0.1%), preventing galvanic carbon pick-up and pitting corrosion on exotic austenitic or duplex steel pipes. Purging tapes maintain air-tight root containment for back-purging oxygen reduction (< 50 PPM) prior to GTAW root deposition.
Technical Focus:Zero Iron Contamination, Diffusible Hydrogen Control, Argon Purge Retention, Loctite Anaerobic Curing.
Explore Other Annexure-1 Consumable Categories
Annexure-112 Items
Cutting, Grinding Wheels & Industrial AbrasivesHigh-speed 4", 5", 7" cutting & grinding discs, polish wheels, and emery papers.
Annexure-19 Items
Industrial Safety Gloves & Personal Protective Equipment (PPE)Heavy leather welding gloves, dotted gloves, 3M goggles, ear plugs & Venus masks.
Annexure-117 Items
Packaging, Purging Tapes, Fasteners & Loctite AdhesivesArgon purging tapes, 6123 masking tapes, Loctite 638/510, rivets, cable ties & MS clips.