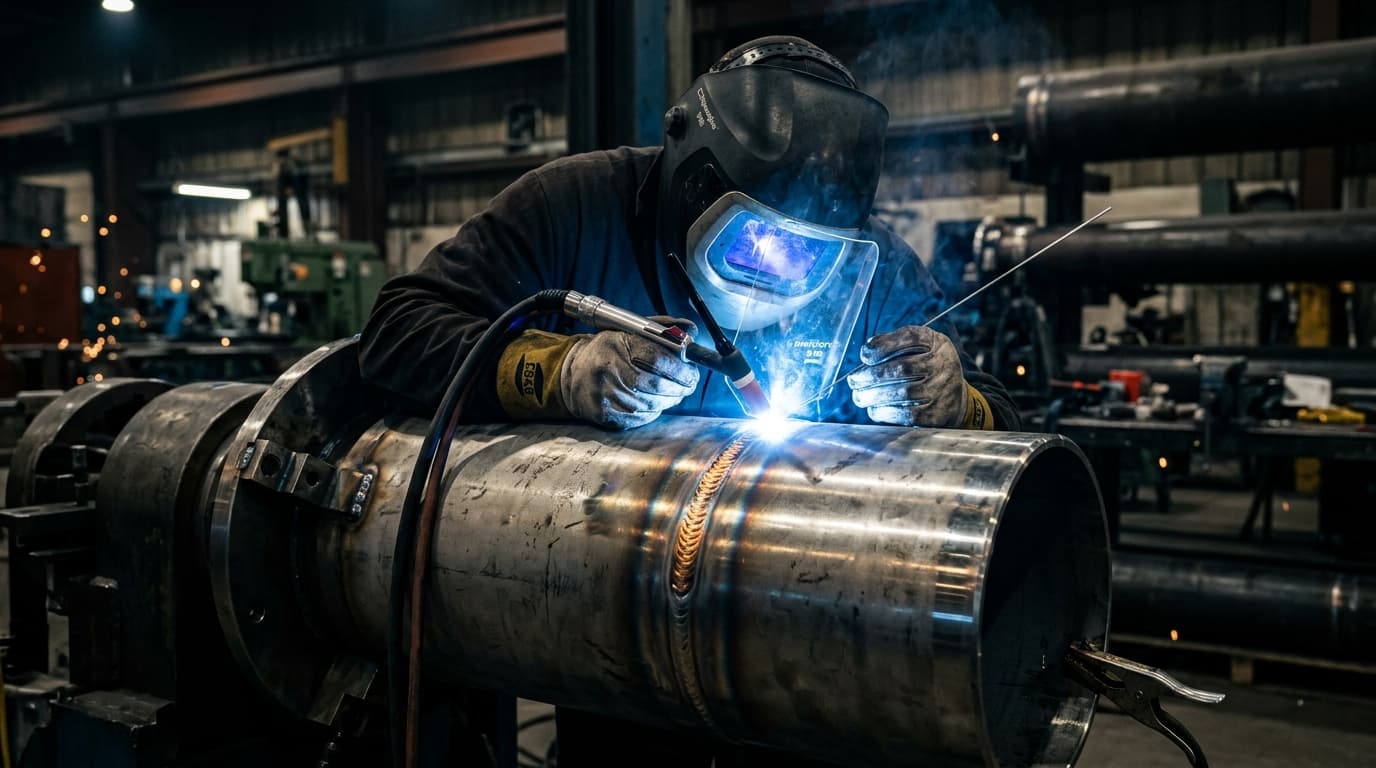
Testing. Consumables.Certified Inspection.
MechSure Engineering Services provides accredited Positive Material Identification (PMI), Fischer Ferritescope FMP30 delta ferrite testing, ASNT Level II NDT, WPS/PQR qualification, and AWS/CSWIP documentation signing — alongside certified Annexure-1 industrial consumables, SS 316L filler wires, 4"/5"/7" cutting & grinding wheels, Loctite compounds, and PPE dispatched from Ulwe, Navi Mumbai.
Industrial Equipment Supply & Certified Technical Solutions
Based in Ulwe, Navi Mumbai, MechSure Engineering Services is an established industrial equipment supplier, consumables stockist, and engineering inspection consultancy. We bridge premium welding hardware with international code compliance.
Led by proprietor Kunda Shivaji Naikade and technical director Sachin Shivaji Naikade (CSWIP 3.1 Certified Welding Inspector, Cert #533022, TWI Certification Ltd Cambridge, UK), we supply heavy-duty Auto ARC & MIG welding machines, pure and thoriated tungsten wires/electrodes, certified low-hydrogen E7018 electrodes, Promotech-style pipe bevelling machinery, and ASME-standard NDT consumables.
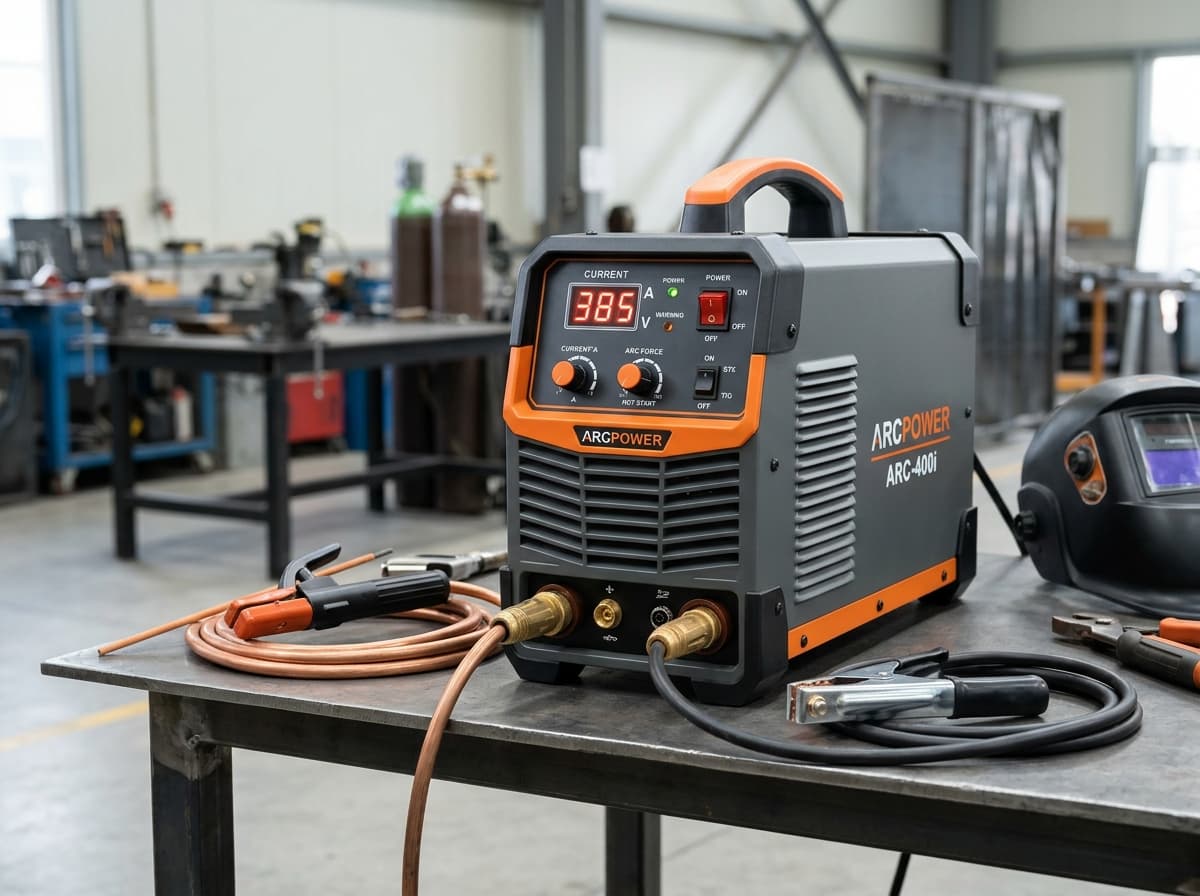
Industrial Products Supply & Certified Inspection Services
We supply industry-leading welding power sources, certified electrodes, Promotech bevelling equipment, and NDT kits — backed by accredited CSWIP 3.1 quality inspection and welding engineering consultancy.
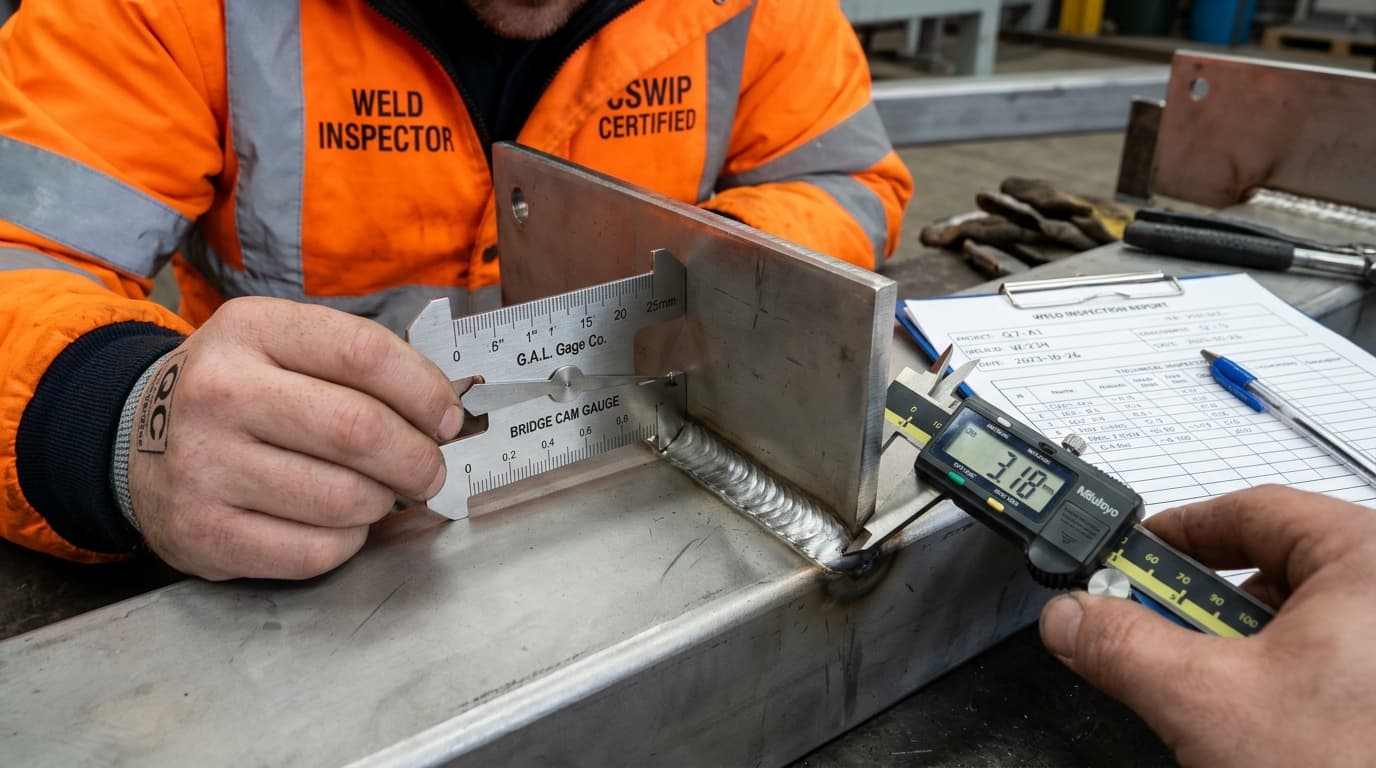
PMI Testing & Level II NDT Inspection
Half Day (200 spots) & Full Day (400 spots) on-site XRF PMI alloy verification within Navi Mumbai & Thane. Multi-method NDT: Liquid Penetrant (DPT), Magnetic Particle (MPT), and Ultrasonic (UT) per shift.
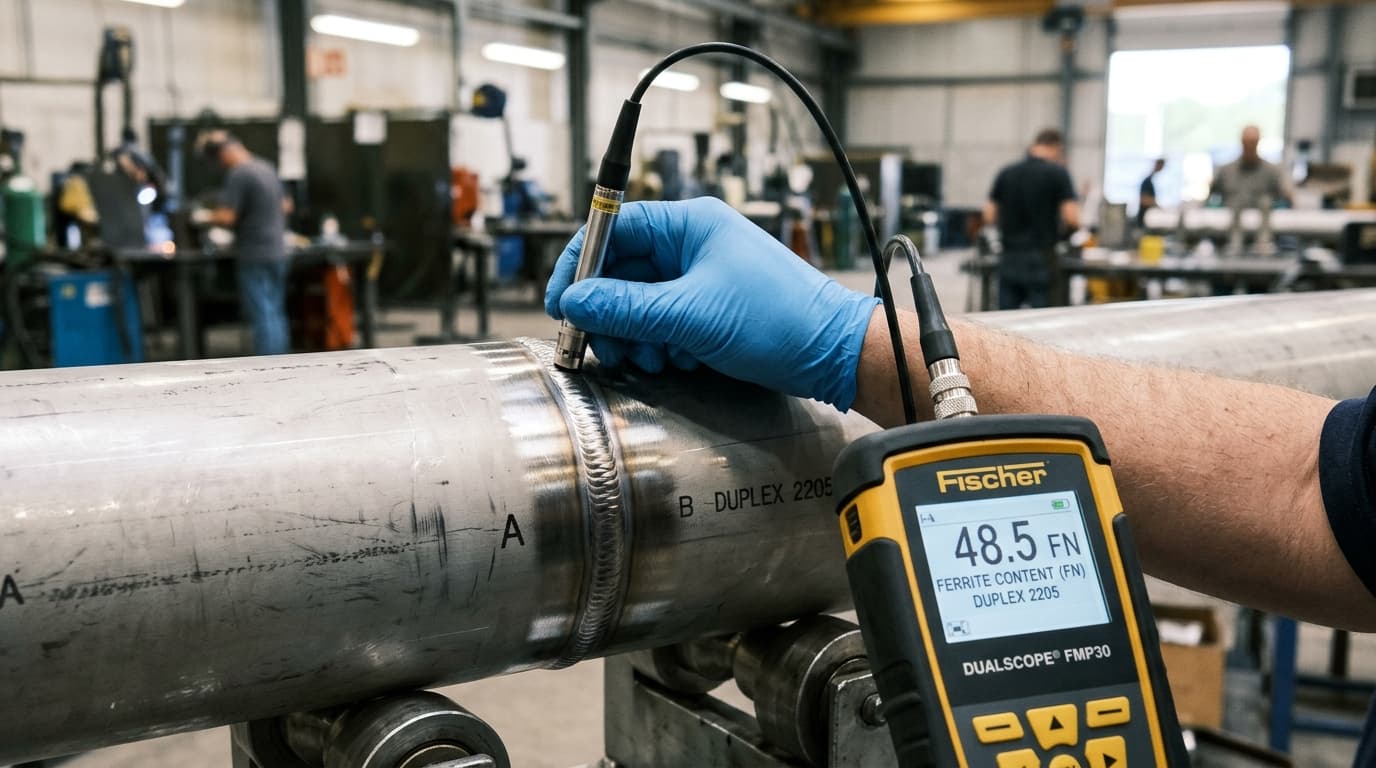
Ferrite Content by Fischer Ferritescope FMP30
Dedicated Per Day (8 Hrs Shift) delta ferrite measurement on duplex 2205, super duplex 2507, and austenitic stainless welds using the genuine Fischer FMP30. AWS A4.2 and ISO 8249 secondary calibration standards.
WPS, PQR, Welder WQTR & Inspector Signing
Complete Welding Procedure Specification (WPS) formulation, PQR test coupon witnessing with NABL labs, 1G to 6G/6GR Welder Qualification (WQTR) with photo ID cards, and AWS CWI & CSWIP 3.1 documentation signing.
Annexure-1 Industrial Consumables Supply
Stockist and distributor of 50+ workshop consumables: 4", 5", 7" cutting & grinding discs, SS 316L (1.6/2.0/2.5mm), ER 70S-6, E 7018, tungsten rods, 14" leather gloves, 3M PPE, purging tapes, and Loctite 638/510.
Looking for specific machine models, tungsten wire diameters, or DPT kits?
The 6-Stage High-Integrity Welding Process
From initial mill certificate verification to final CSWIP 3.1 inspection sign-off, every welded joint and machined component moves through verifiable quality hold points.
Drawing Review & WPS Formulation
Review of engineering drawings, code requirements (ASME Sec IX / AWS D1.1), base metallurgy, and joint geometry. Formulation of verified Welding Procedure Specifications (WPS).
Material Receipt & 3.1 Traceability
Physical inspection of mill plates, pipes, and filler consumables. Heat numbers cross-referenced to EN 10204 Type 3.1 mill test certificates and hard-stamped.
Bevel Preparation & Fit-Up Check
Precision beveling (60° inclusive / J-prep), root face, and root gap verification using calibrated Bridge Cam and Hi-Lo gauges. Tacks welded to WPS criteria.
Argon Back-Purge Residual O₂ Check
For stainless and duplex lines, inflatable purge dams isolate the internal pipe volume. Continuous digital oxygen analysis guarantees residual O₂ < 50 PPM before arc strike.
Controlled Fusion & Interpass Monitoring
Multi-pass GTAW / GMAW welding with continuous contact pyrometer verification. Interpass temperature maintained strictly under 150°C for stainless and 100°C for duplex.
CSWIP 3.1 VT & Pressure Hydrotest
100% visual examination by CSWIP 3.1 inspector (Cert #533022) to BS EN ISO 17637 Quality Level B, hydrostatic pressure testing up to 350 bar, and full QA dossier handover.
Engineered for Mission-Critical Operating Environments
Our fusion welding and component fabrication procedures meet the rigorous compliance standards of multinational industrial clients and engineering consultants.
Oil & Gas Refineries & Piping
High-pressure hydrocarbon process lines, duplex 2205 manifolds, and ANSI B16.5 flanged pipe spools engineered for sour gas and offshore corrosive environments.
Chemical & Petrochemical Processing
Inconel 625, Hastelloy C-276, and austenitic stainless reaction vessels, columns, and heat exchanger tube-to-tubesheet precision TIG welding.
Pharmaceutical & Sanitary CIP Skids
Clean-in-place sanitary tubing with automated orbital/manual TIG welding, monitored residual O₂ < 50 PPM, and electro-polished Ra < 0.4 µm interior finish.
Heavy Mechanical OEM & Equipment
Vibration-resistant structural bases for compressor skids, heavy hydraulic pump units, gearbox frames, and CNC-machined bearing brackets.
Power Generation & Pressure Vessels
ASME Section VIII Div 1 pressure vessels, steam drums, and boiler headers using ASTM A516 Gr 70 plate with multi-pass volumetric NDT qualification.
Offshore Marine & Transport
Heavy marine lifting frames, 5083 aluminium marine fuel tanks, and subsea structural members tested under third-party marine classification societies.
Critical Industrial Assemblies Built & Inspected
Real component manufacturing examples illustrating our high-integrity welding, CNC precision machining, and strict adherence to global engineering codes.
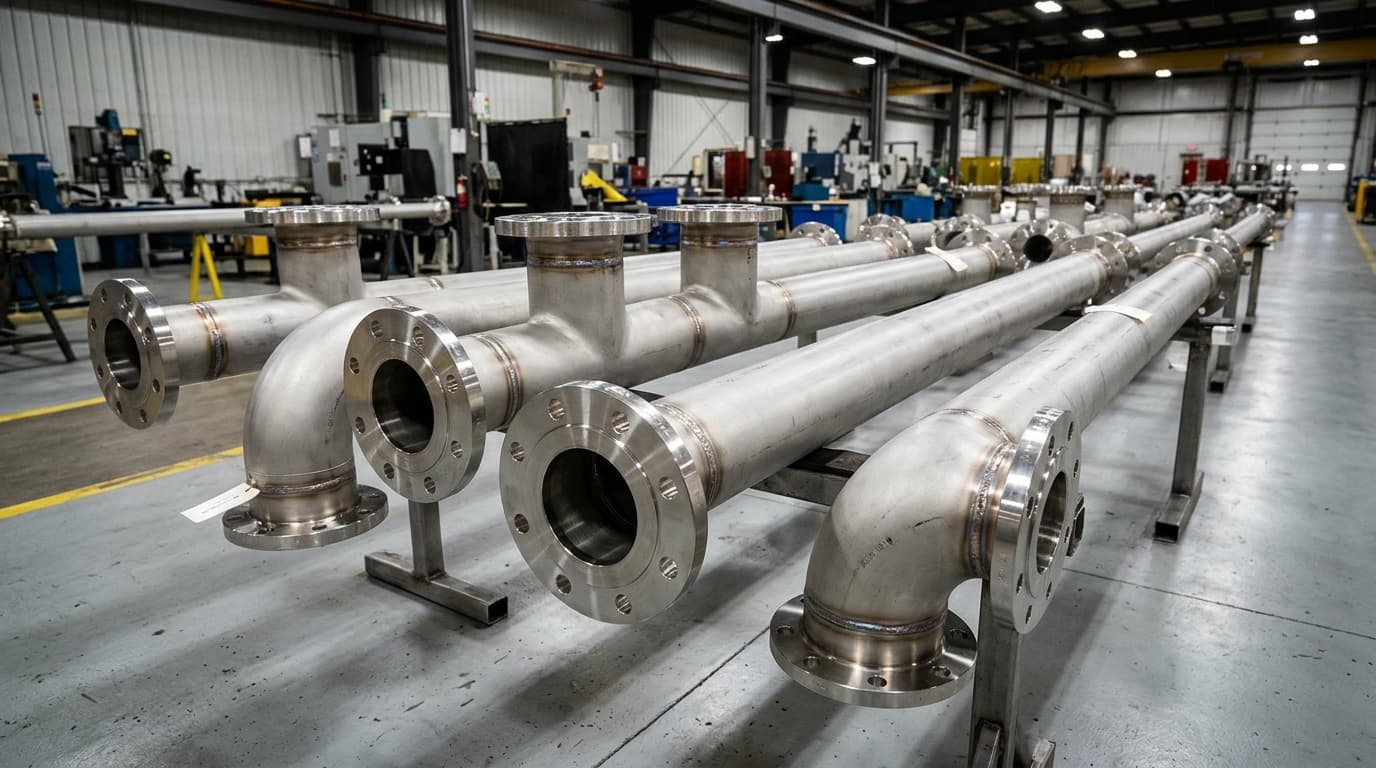
High-Pressure Duplex 2205 Process Spools
Fabricated high-pressure offshore process spools with welded weldolets and ANSI B16.5 flanges. Argon back-purging monitored continuously below 50 PPM O₂, with zero internal sugaring and 100% radiographic acceptance.
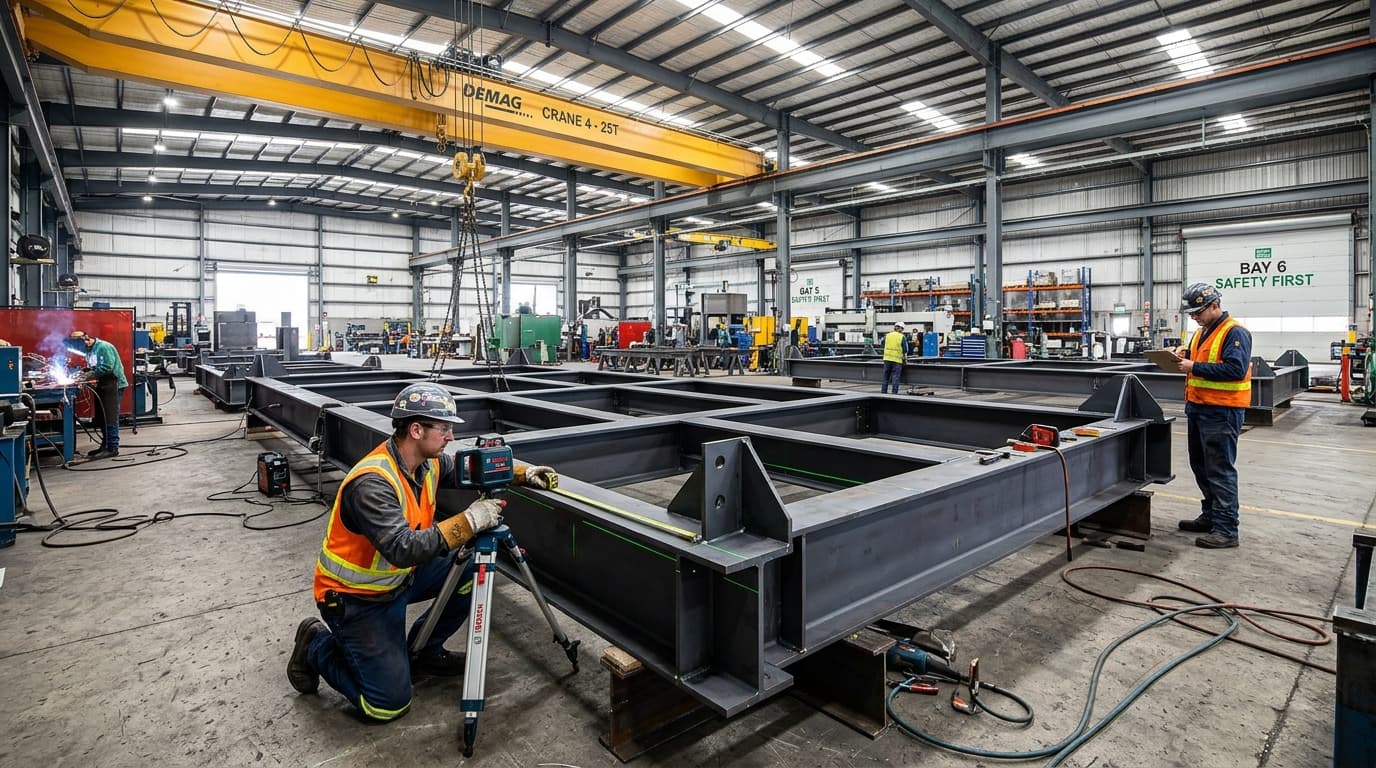
Heavy Structural Compressor Skid Package
Fabricated heavy vibration-damped structural skid frame for multi-stage gas compressor. 3D fixtured to maintain levelness within ±0.25mm across 4.5 meters. Fully MPI tested per AWS D1.1.
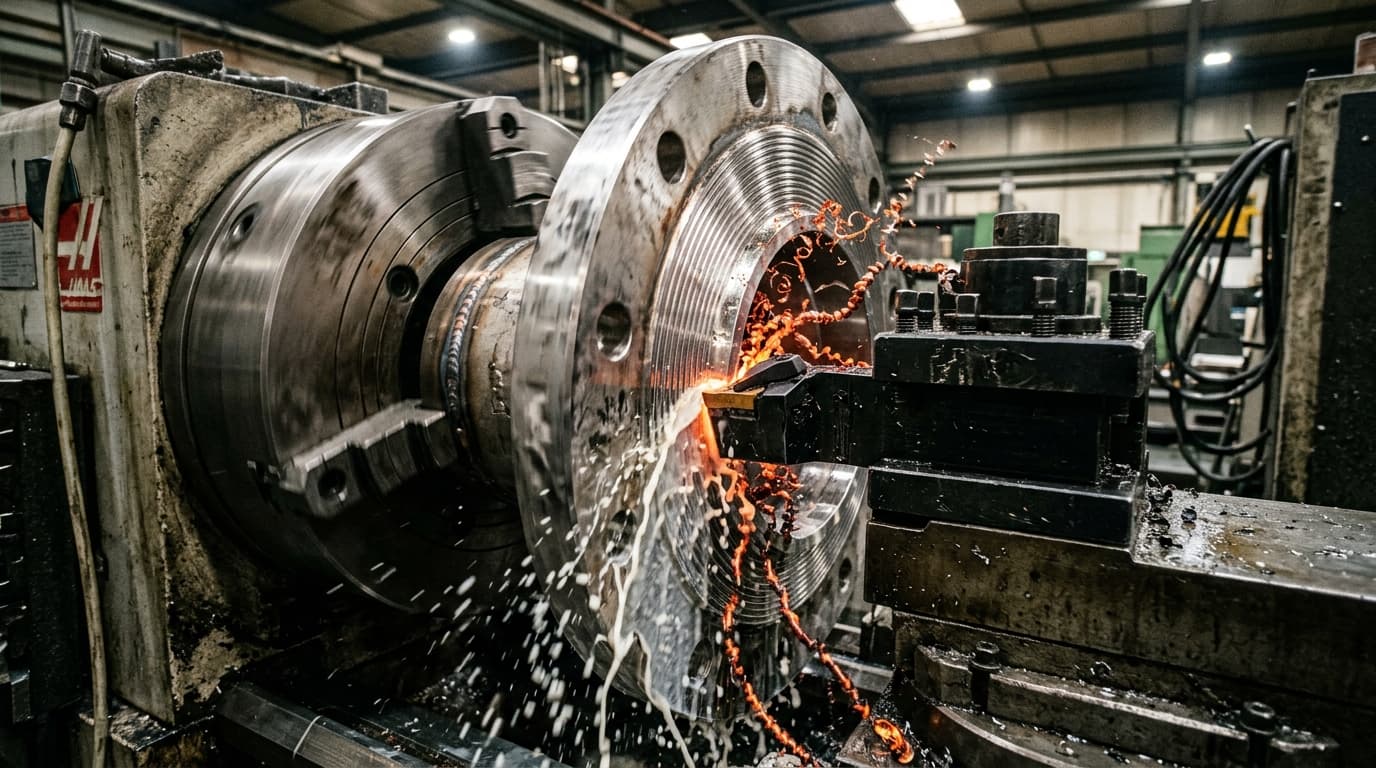
Custom CNC Lathed Weld-Neck Flange Manifold
Complex manifold with 6 socket-welded branch connections. Flange raised faces CNC finish-machined post-welding to eliminate angular distortion and guarantee Ra 3.2 µm sealing finish.
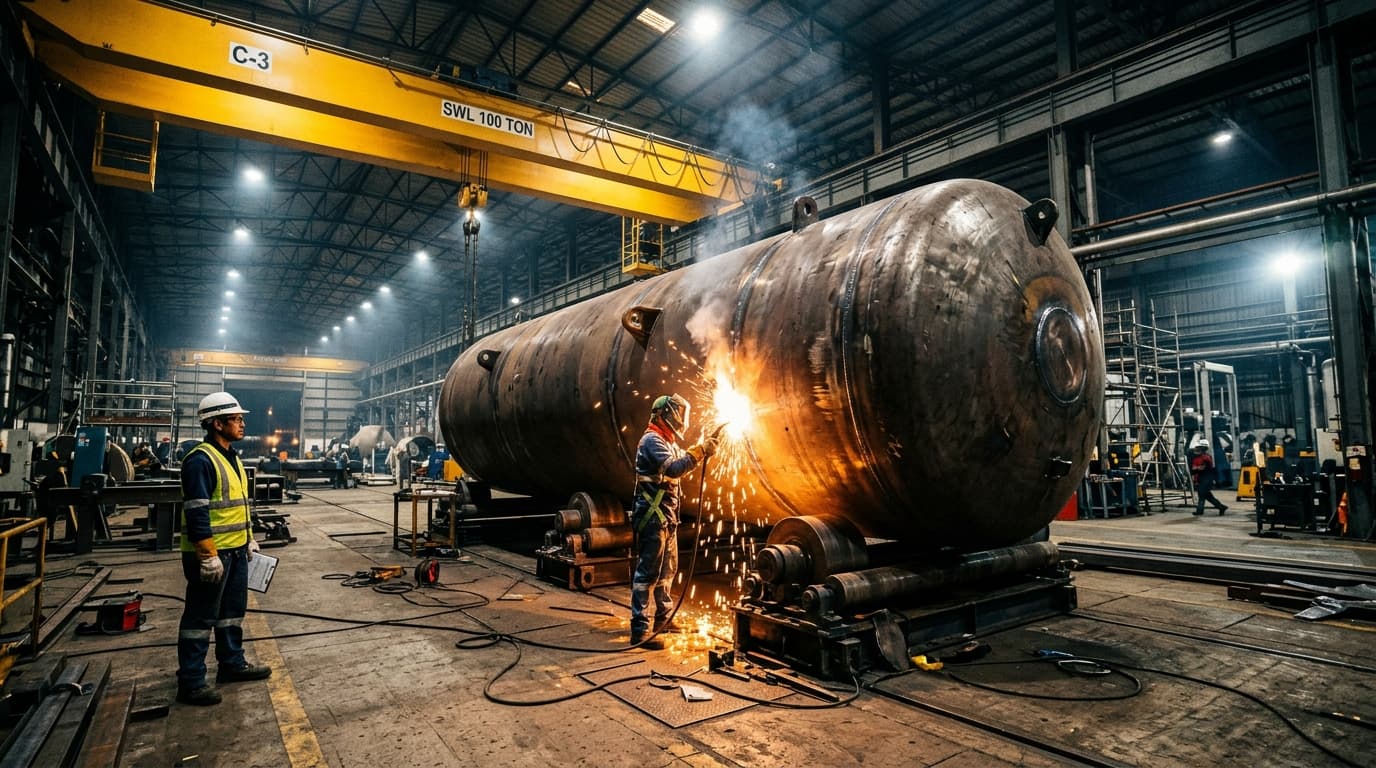
Boiler Quality Pressure Vessel Shell Seams
Multi-pass submerged arc and synergic GMAW circumferential seams on thick-wall pressure vessel cylinders. Qualified strictly to ASME Section VIII Div 1 with full ultrasonic examination.
International Code Compliance & Zero-Defect Standards
We eliminate costly weld failures and client audit non-conformances by enforcing internationally recognized standards across all shop and field operations.
Welding procedure specifications (WPS), procedure qualification records (PQR), and welder performance qualifications (WPQ).
Governs 100% of our pre-weld fit-up, root pass inspection, and final weld cap profile examination to Quality Level B.
Structural steel framework, skid bases, and crane gantries fabricated with controlled preheat and interpass heat inputs.
Complete mill test certificates validating tensile strength, chemical composition, and heat number hard stamping on all components.
How We Deliver Industrial Assurance
Rather than generic claims, our operations are bound by measurable engineering commitments that safeguard your critical infrastructure against downtime and weld failures.
Zero-Defect Culture
Rework delays client delivery schedules. By enforcing strict pre-weld joint prep, calibrated bevel angles, and argon back-purge oxygen verification below 50 PPM, our first-pass radiographic and visual pass rate exceeds 99.2%.
Complete Material Traceability
Every pipe length, forged flange, and welding filler wire is matched directly to authentic EN 10204 Type 3.1 mill inspection certificates. Heat numbers are hard-stamped or etched on dispatched components.
Certified Inspector Supervision
Our welders do not work in isolation. Every weld joint fit-up, root pass, and final cap profile is monitored and signed off by Sachin Shivaji Naikade (CSWIP 3.1 Cert No: 533022, TWI Cambridge UK).
24-Hour RFQ & Emergency Mobilization
We provide comprehensive engineering review and quote feedback within 24 hours. For critical plant shutdowns in Maharashtra industrial zones, our field welding squad deploys on a 24/7 on-call basis.
Let's Build Something That Lasts.
Connect directly with Sachin Shivaji Naikade (CSWIP 3.1) and our fabrication engineers. We review technical specifications and provide quotation assessments within 24 hours.
Request a Technical Quotation (RFQ)
Provide your project specifications and requirements for an engineering review.