Back to All Consumables & Supplies
Annexure-1 Certified • High RPM Tested
Cutting, Grinding Wheels & Industrial Abrasives
Premium reinforced cutting wheels, heavy stock-removal grinding discs, 80 & 120 grit polish paper wheels, and bimetal hacksaw blades engineered for stainless steel and structural fabrication.
Annexure-1 Items: 12 Verified Products
Dispatch Hub: Sector-20, Ulwe, Navi Mumbai
QA Vetting: CSWIP 3.1 • EN 10204 3.1
Annexure-1 Dimensional & Size Schedule
12 items cataloged| Item # | Item Description | Size / Dimension | Grade / Brand Ref | MTR Status |
|---|---|---|---|---|
| #1 | Cutting Wheel 5" (125 x 3.2 x 22.23) | 125 X 3.2 X 22.23 mm | Annexure-1 / Norton Industrial Grade | EN 10204 3.1 |
| #2 | Cutting Wheel 7" (180 x 2.8 x 22.23) | 180 X 2.8 X 22.23 mm | Annexure-1 / Norton Industrial Grade | EN 10204 3.1 |
| #34 | Cutting Wheel 4" Standard (100 x 2.5 x 16) | 100 X 2.5 X 16 mm | Annexure-1 / Industrial Grade | EN 10204 3.1 |
| #35 | Cutting Wheel 4" Thin (100 x 1.0 x 16 - 1 mm Thick) | 100 X 1.0 X 16 mm (1 mm thick) | Annexure-1 / Inox Premium | EN 10204 3.1 |
| #3 | Grinding Wheel 4" (100 x 4 x 16) | 100 X 4 X 16 mm | Annexure-1 / Norton Industrial Grade | EN 10204 3.1 |
| #4 | Grinding Wheel 5" (125 x 6 x 22.23) | 125 X 6 X 22.23 mm | Annexure-1 / Norton Industrial Grade | EN 10204 3.1 |
| #5 | Grinding Wheel 7" (180 x 6.7 x 22.23) | 180 X 6.7 X 22.23 mm | Annexure-1 / Norton Industrial Grade | EN 10204 3.1 |
| #6 | Polish Paper Wheel 1" (25 x 25 x 80 Grit) | 25 X 25 X 80 GRIT (1 Inch Spindle Wheel) | Annexure-1 / CUMI / Abrasives | EN 10204 3.1 |
| #7 | Polish Paper Wheel 4" (4" x 80 Grit) | 4" X 80 GRIT (Flap Disc) | Annexure-1 / CUMI / Abrasives | EN 10204 3.1 |
| #9 | Polish Paper Sheet - 80 Grit (No. 80) | Standard Sheet (NO. 80 Grit) | Annexure-1 / CUMI Polish Paper | EN 10204 3.1 |
| #8 | Polish Paper Sheet - 120 Grit (No. 120) | Standard Sheet (NO. 120 Grit) | Annexure-1 / CUMI Polish Paper | EN 10204 3.1 |
| #38 | Generic Consumable: Hacksaw Blade 12" | 12" (300 mm) Length | Annexure-1 / Industrial Grade | EN 10204 3.1 |
Individual Product Profiles & Specifications
12 verified industrial items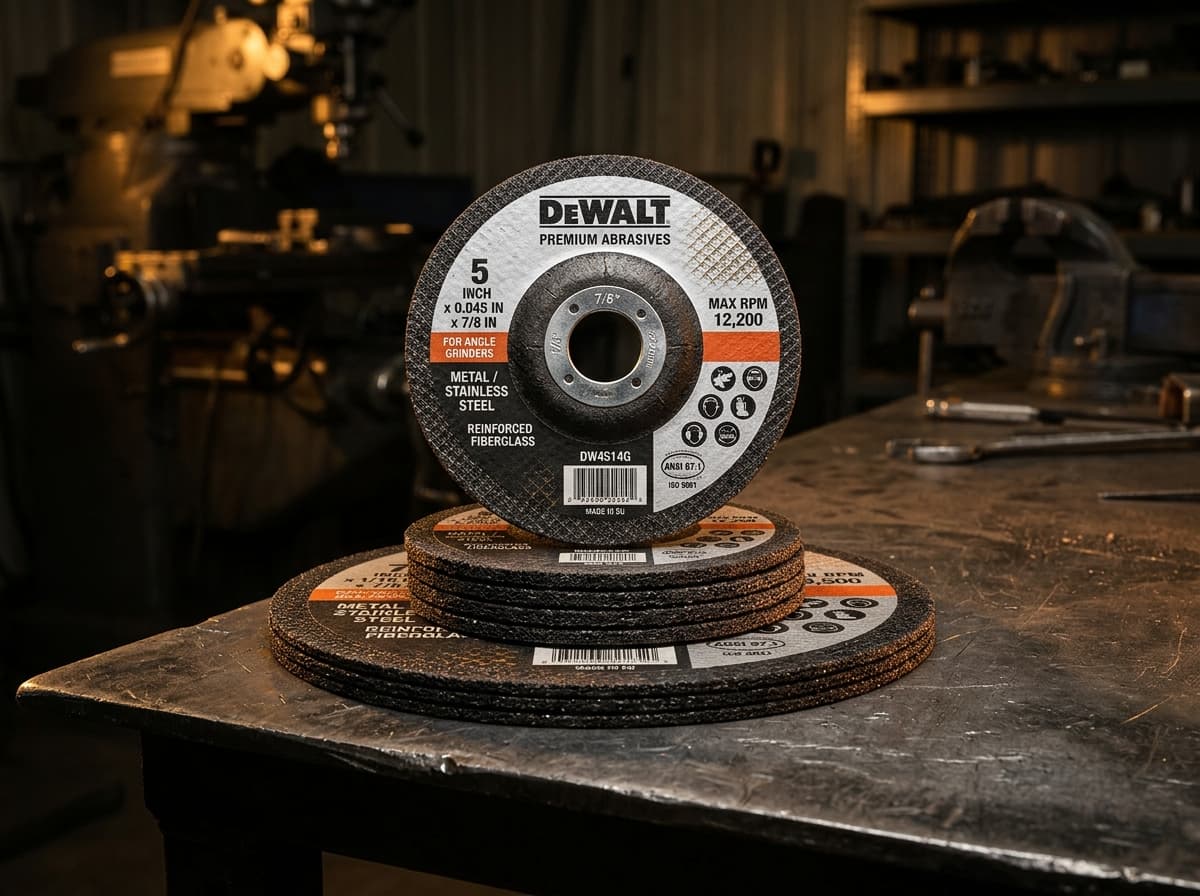
Fast Moving
Cutting
Cutting Wheel 5" (125 x 3.2 x 22.23)
Heavy duty 5" abrasive cutoff wheel for stainless steel and carbon steel pipe/plate slicing.
- Ultra-fast slicing with minimal burr formation
- Low iron, sulfur, and chlorine (< 0.1%) to prevent stainless steel contamination
- Engineered for heavy-duty chop and handheld cutting
Fast Moving
Cutting
Cutting Wheel 7" (180 x 2.8 x 22.23)
High capacity 7" cutoff wheel for thick structural steel beams and heavy wall piping.
- Extended disc longevity in heavy continuous fabrication
- High lateral stability resisting side twisting loads
- Minimal thermal burn and discoloration on carbon and alloy steels
Cutting
Cutting Wheel 4" Standard (100 x 2.5 x 16)
Universal 4" cutoff wheel for 100mm compact angle grinders across general fabrication.
- Reliable cutting rate on general carbon steels
- Reinforced against edge chipping
- Compatible with all 4" standard Indian grinders
Fast Moving
Cutting
Cutting Wheel 4" Thin (100 x 1.0 x 16 - 1 mm Thick)
Ultra-thin 1mm Inox cutting wheel for razor-sharp, burr-free cuts on thin SS tubes and sheets.
- Extremely cool cutting preventing heat-affected zone (HAZ) damage
- Requires minimal tool pressure, reducing operator fatigue
- Leaves mirror-smooth edges ready for TIG autogenous welding
Cutting
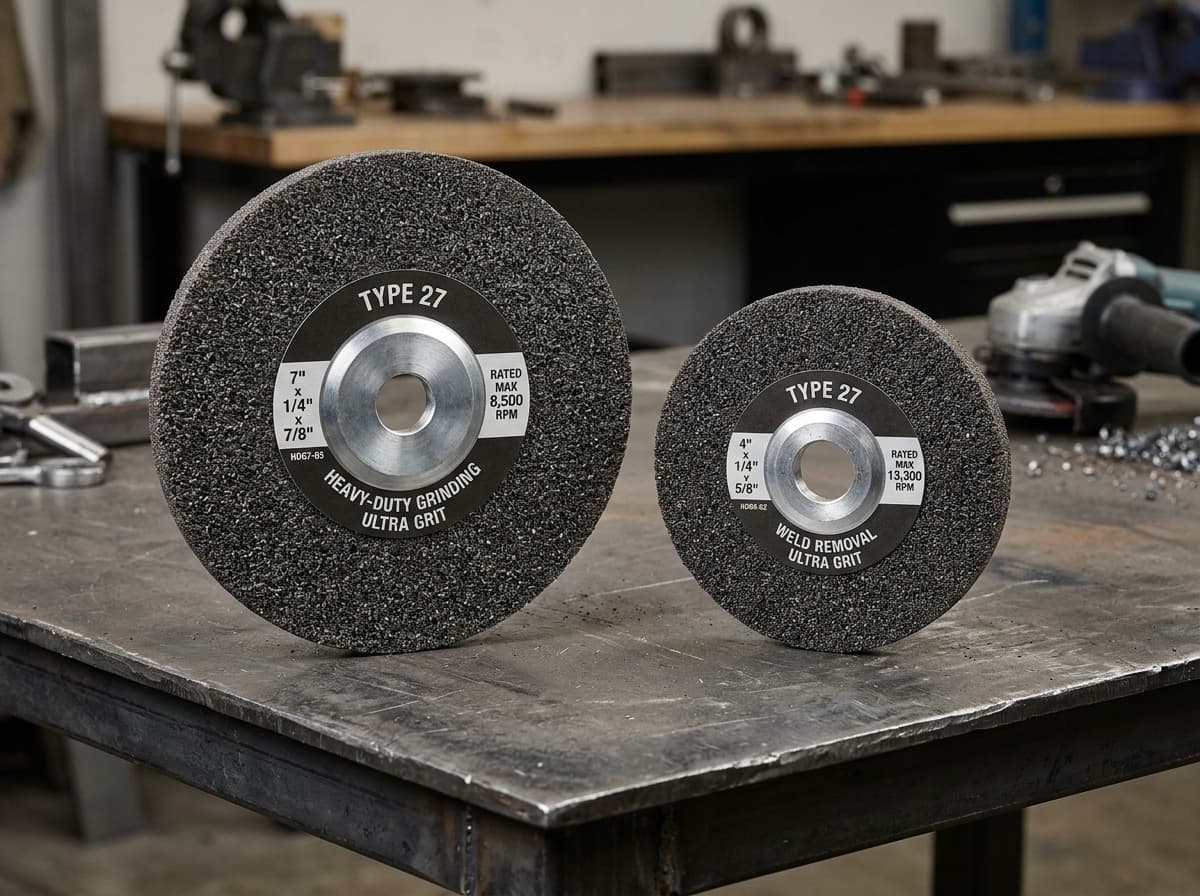
Grinding Wheel 4" (100 x 4 x 16)
Compact 4" depressed-center grinding wheel (DCD) for weld seam deburring and bevel dressing.
- Smooth vibration-free grinding action
- High material removal rate on weld caps and bevels
- Long service life without premature glazing
Fast Moving
Cutting
Grinding Wheel 5" (125 x 6 x 22.23)
Heavy duty 5" grinding disc (6mm thick) for aggressive stock removal on structural steel.
- Maximum stock removal rate for industrial heavy engineering
- Triple fiberglass reinforcement for extreme operator safety
- Consistent wear profile with low vibration
Cutting
Grinding Wheel 7" (180 x 6.7 x 22.23)
Extra heavy duty 7" grinding wheel (6.7mm thick) for large pressure vessel and shipyard welds.
- Maximum durability under continuous industrial duty
- Resists edge crumble during aggressive gouging cleanup
- Cool cutting formulation preventing metallurgical overheating
Cutting
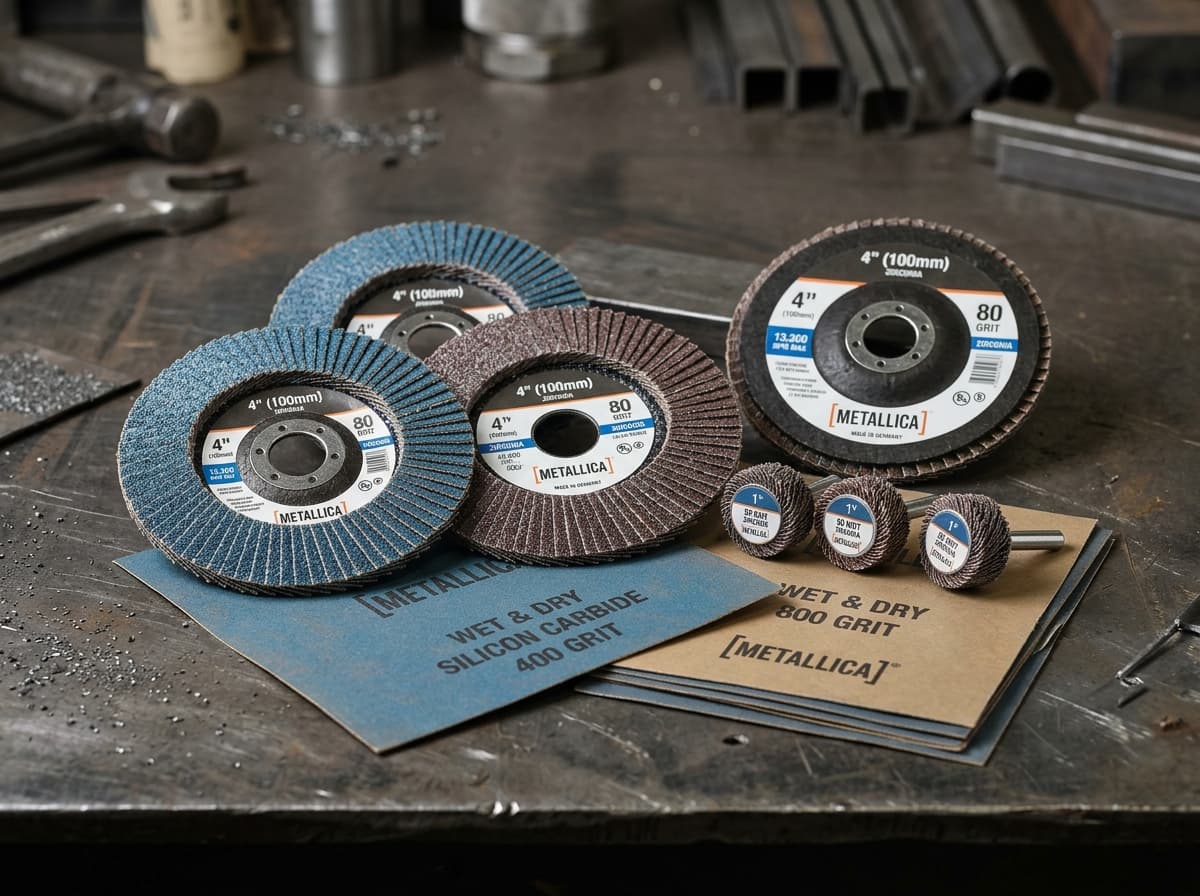
Polish Paper Wheel 1" (25 x 25 x 80 Grit)
Mounted flap/polish paper wheel (80 grit) for intricate tube ID and bore polishing.
- Flexible abrasive cloth leaves consistent linear finish
- Accesses tight internal diameters and valve seat pockets
- Uniform grain wear for long operating life
Fast Moving
Cutting
Polish Paper Wheel 4" (4" x 80 Grit)
Abrasive flap disc wheel 4" (80 grit) for one-step weld blending and surface finishing.
- One-step grinding and finishing replaces separate discs
- Reduced operator fatigue compared to rigid grinding wheels
- Leaves smooth surface ready for paint or dye penetrant inspection
Cutting
Polish Paper Sheet - 80 Grit (No. 80)
Heavy-duty waterproof emery polish paper sheet (80 grit) for rough surface smoothing.
- Wet and dry application versatility
- Resistant to paper tearing and curling
- Fast cut on stainless steel, brass, and alloy steels
Cutting
Polish Paper Sheet - 120 Grit (No. 120)
Fine waterproof polish paper sheet (120 grit) for satin finishing and inspection prep.
- Provides uniform micro-scratch profile
- Essential for preparing weld toes for CSWIP visual inspection
- High flexibility around cylindrical pipe curves
Cutting
Generic Consumable: Hacksaw Blade 12"
Bimetal high-speed steel (HSS) 12" hand hacksaw blade for precise manual metal sawing.
- Virtually unbreakable under heavy manual tension
- High tooth hardness retaining sharp edge across hard metals
- Standard pinhole fit for all industrial hacksaw frames
Technical Documentation • Annexure-1 Engineering Standards
Engineering Notes for Cutting, Grinding Wheels & Industrial Abrasives
Quality Assurance, Heat Traceability & EN 10204 3.1 Certificates
In high-integrity engineering applications across Navi Mumbai, Taloja, Rabale, and Maharashtra fabrication corridors, consumable quality directly dictates weld longevity and safety. MechSure Engineering guarantees that all supplied welding wires, electrodes, abrasives, and chemical sealing products are authenticated against mill test certificates (MTR).
Every batch of SS 316L filler wire, ER 70S-6 MIG spools, and E 7018 basic low-hydrogen electrodes is traced by heat number, documenting exact chemical composition (C, Mn, Si, P, S, Cr, Ni, Mo, N) and mechanical properties (Tensile strength, Yield strength, Elongation %, and Charpy V-Notch impact values at -30°C or -46°C).
Applicable Codes:AWS A5.9, AWS A5.18, AWS A5.1, ASME Section II Part C, EN 10204 3.1/3.2, IS 814.
Handling, Storage & Shop-Floor Best Practices
Proper storage and application discipline ensure peak consumable performance. Low-hydrogen E 7018 electrodes must be maintained in holding ovens at 120°C to 150°C after re-baking to prevent hydrogen-induced cold cracking (HICC) in high-strength structural joints.
For stainless steel cutting and grinding, our cutting wheels (125 x 3.2, 180 x 2.8, 100 x 1.0) are strictly formulated free of iron, sulfur, and chlorine (< 0.1%), preventing galvanic carbon pick-up and pitting corrosion on exotic austenitic or duplex steel pipes. Purging tapes maintain air-tight root containment for back-purging oxygen reduction (< 50 PPM) prior to GTAW root deposition.
Technical Focus:Zero Iron Contamination, Diffusible Hydrogen Control, Argon Purge Retention, Loctite Anaerobic Curing.
Explore Other Annexure-1 Consumable Categories
Annexure-114 Items
Welding Filler Wires, Electrodes & TungstenCertified SS 316L, ER 70S-6 MIG, ER 70S-2 TIG, E 7018 & Tungsten rods.
Annexure-19 Items
Industrial Safety Gloves & Personal Protective Equipment (PPE)Heavy leather welding gloves, dotted gloves, 3M goggles, ear plugs & Venus masks.
Annexure-117 Items
Packaging, Purging Tapes, Fasteners & Loctite AdhesivesArgon purging tapes, 6123 masking tapes, Loctite 638/510, rivets, cable ties & MS clips.